

Home Chemical & Industrial Chemical Pumping & Controls Multifunctional Controller
Multifunctional Controller
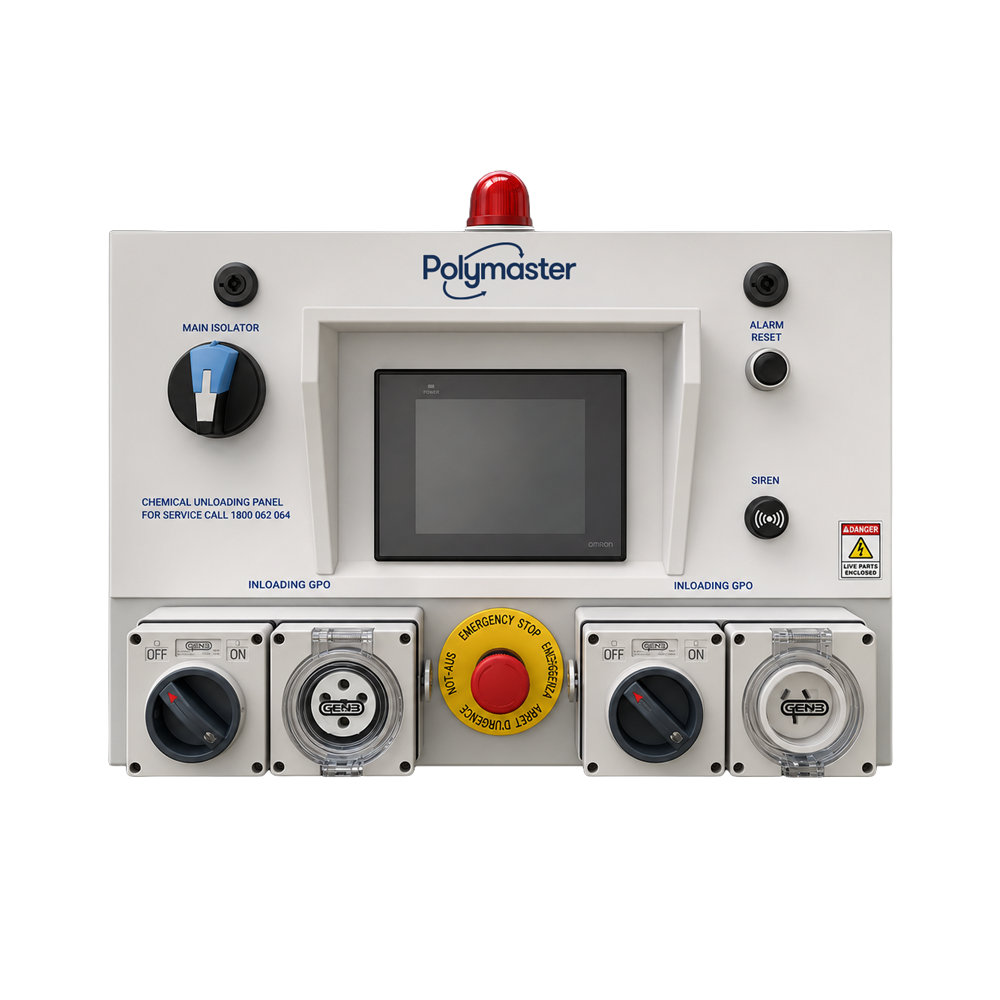
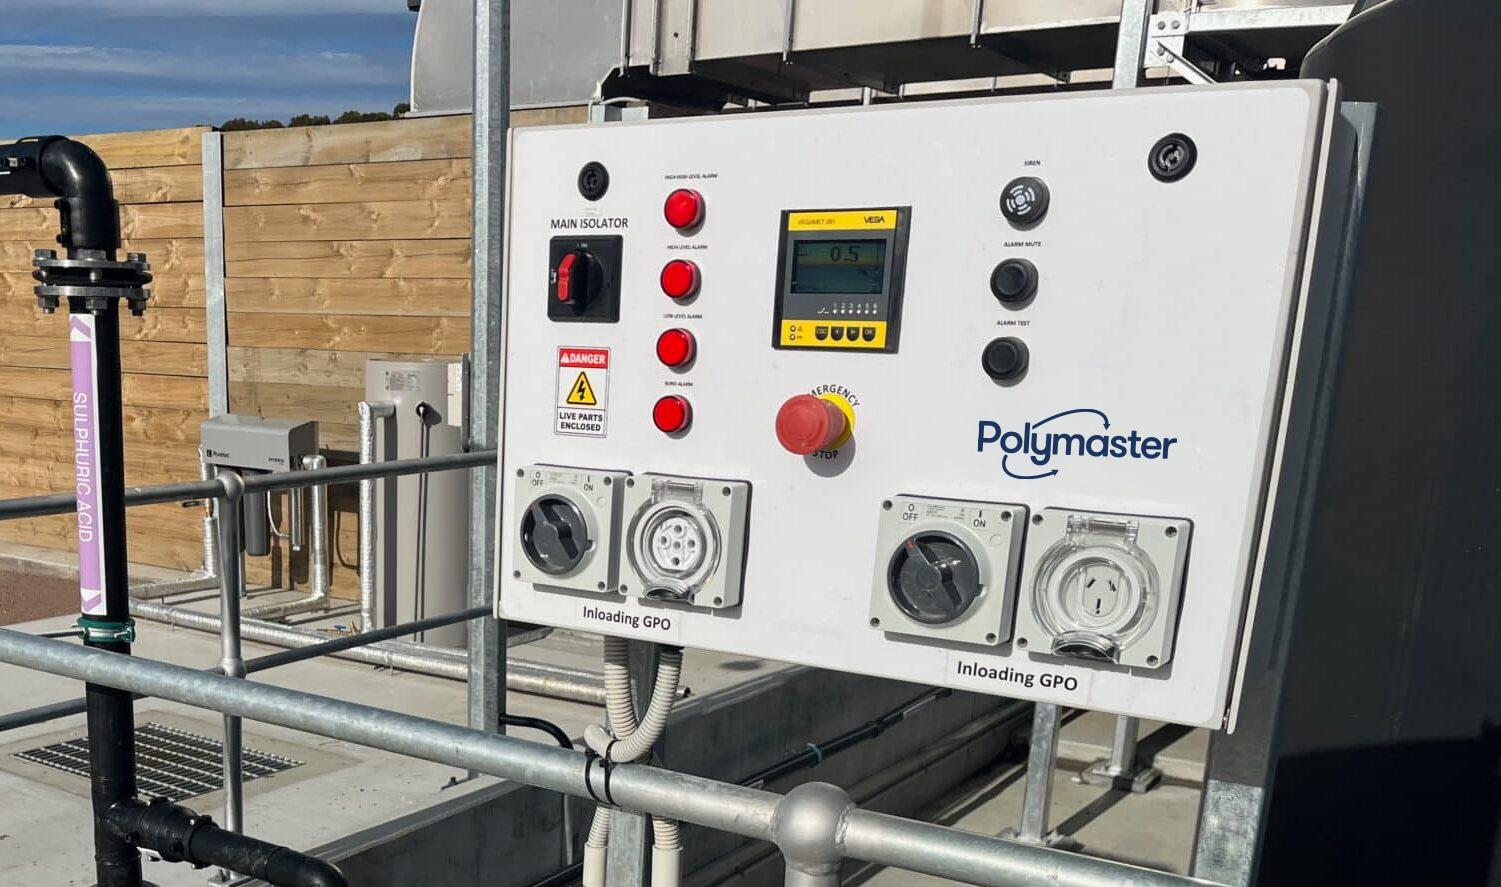
The Multifunctional Controller is a versatile and innovative component designed to seamlessly integrate into a wide range of industrial applications. It manages the safe and efficient transfer of chemicals, wastewater, and other substances.
Seamlessly Manage Chemical Transfers and Control with the Multifunctional Controller
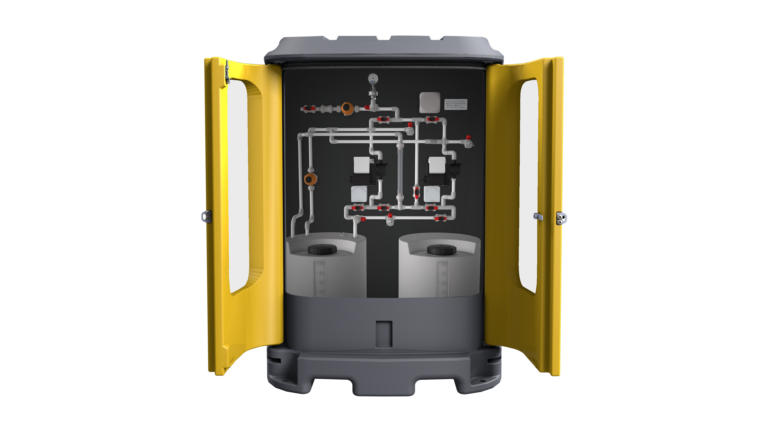
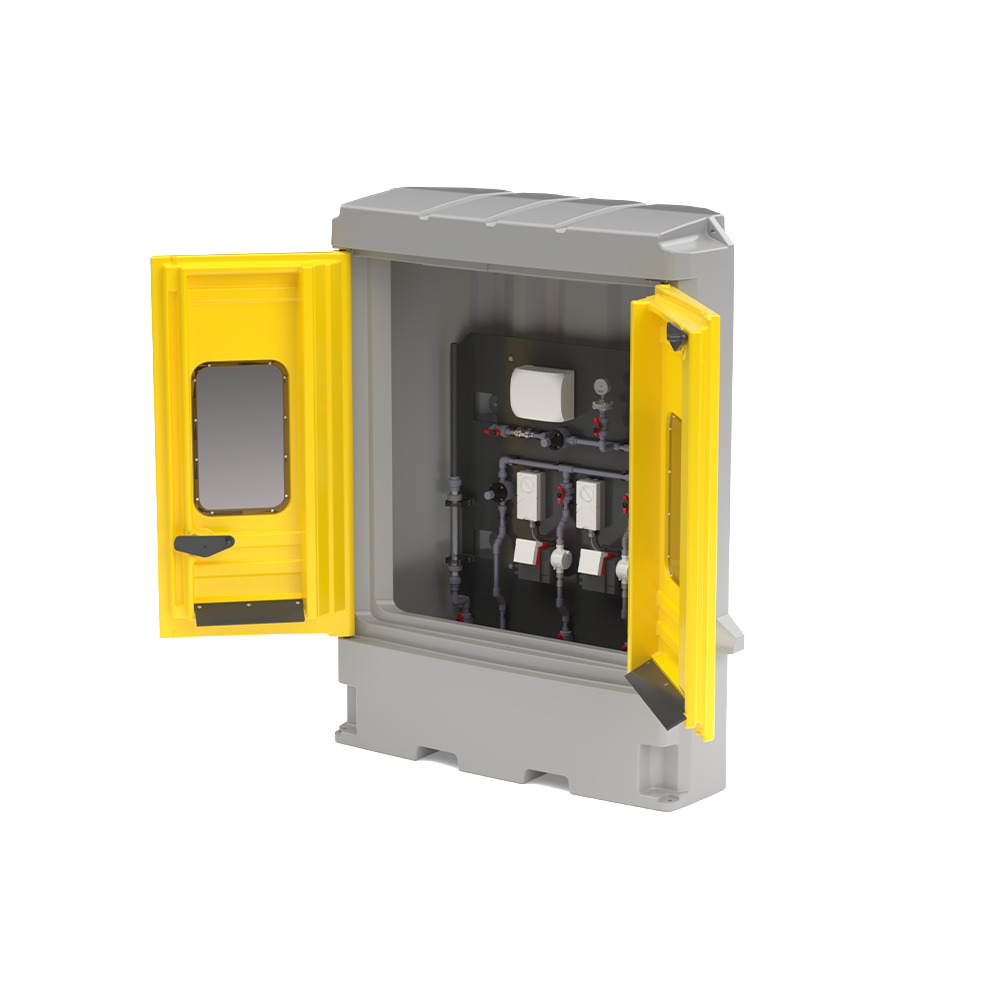
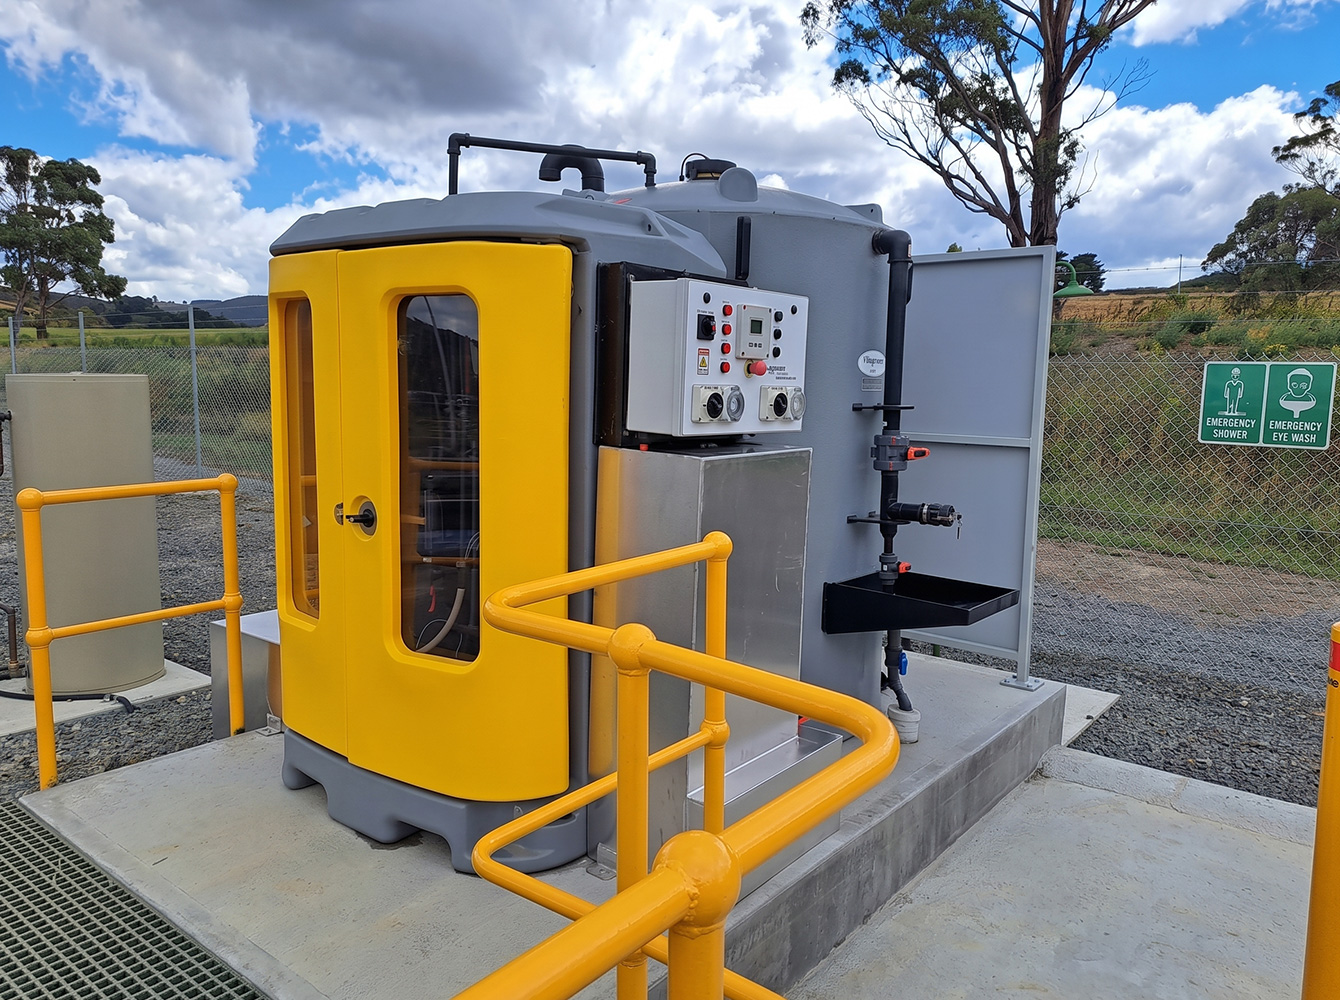
The Multifunctional Controller is a versatile and innovative component designed to seamlessly integrate into a wide range of industrial applications. It manages the safe and efficient transfer of chemicals, wastewater, and other substances.This essential component forms a core part of systems such as the Chemical Transfer Station and the Chemical Unloading / Truckfill Station.
The controller is built with advanced features that ensure smooth operations, prioritising both safety and reliability. Whether it’s controlling chemical transfers, managing truck unloading, or enabling future capabilities like dosing control, the Multifunctional Controller adapts to meet the demands of various industrial processes.
Key Benefits
Automated Control
- The Multifunctional Controller automates chemical transfer processes, minimising manual intervention and enhancing operational efficiency.
Advanced Safety Systems
- Built-in alarms, emergency stop functions, and dual redundancy sensors ensure safety, reducing risks of overfills, spills, and equipment damage.
Remote Monitoring and Control
- Operators can monitor and control the system remotely through multiple interface outputs, allowing real-time data access and proactive maintenance.
Customisable and Expandable
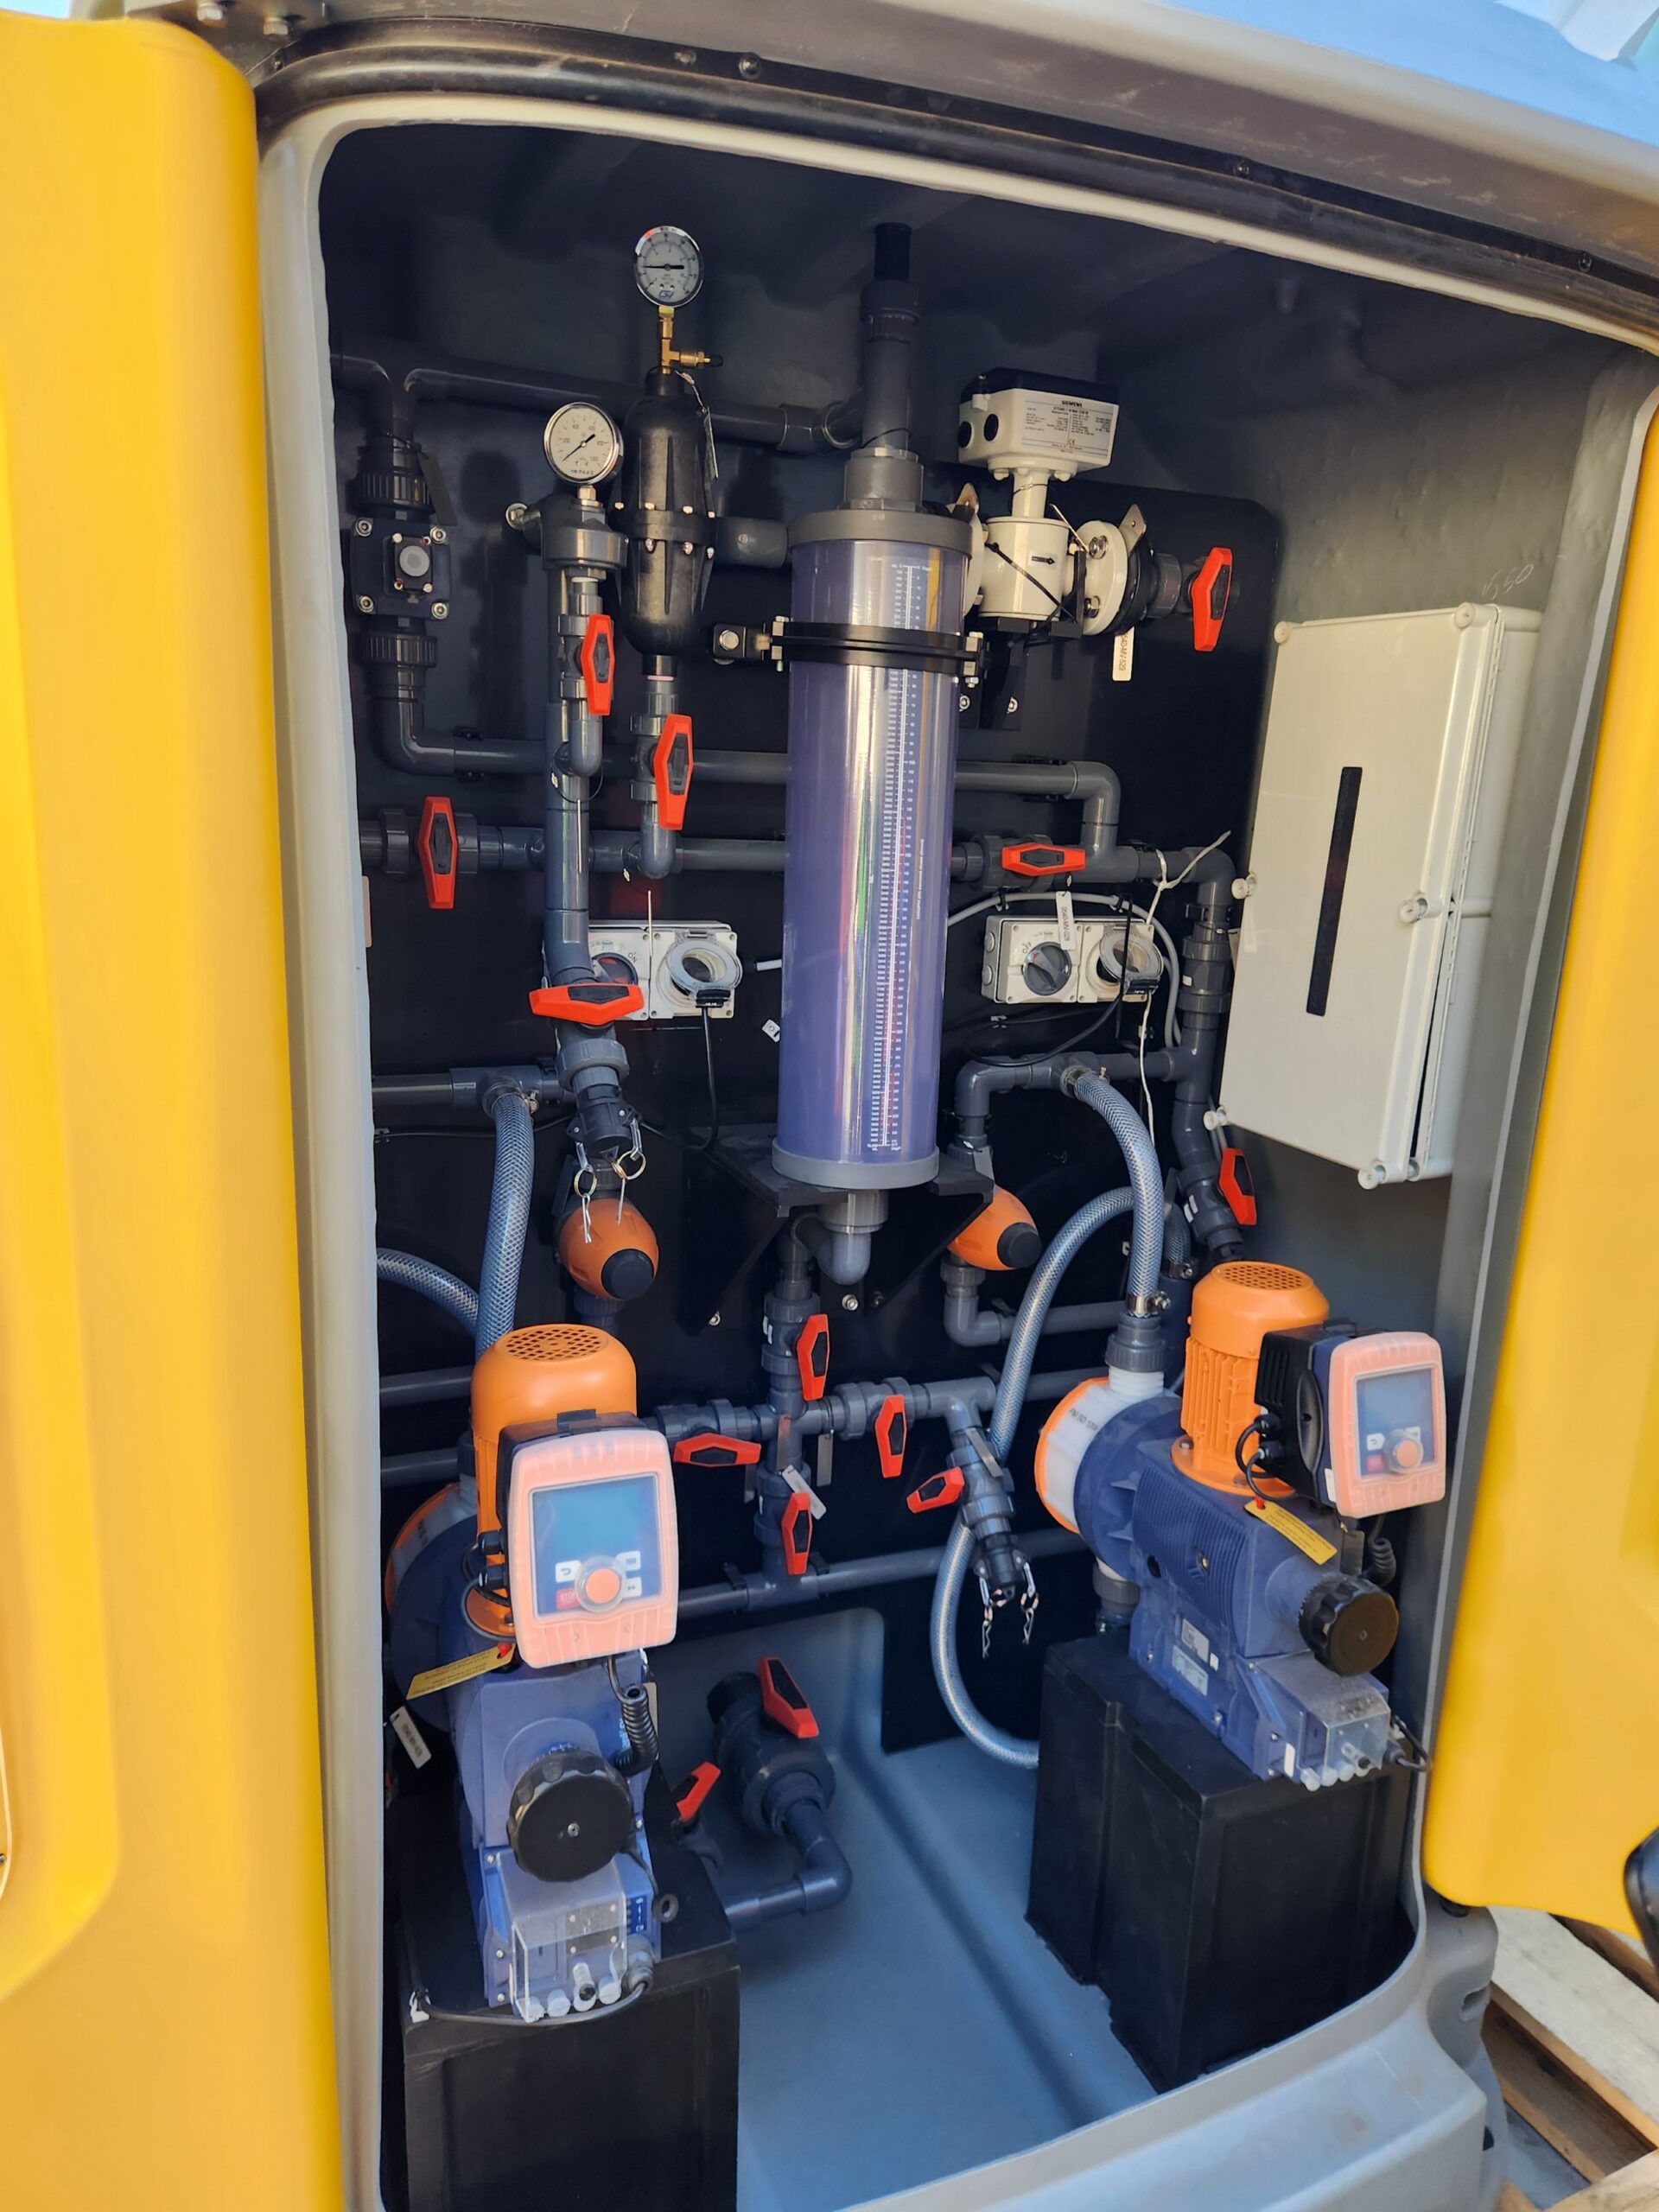
- It can be tailored with various accessories such as pumps, cabinets, and piping.
- Future software upgrades expand its capabilities to include pH and chlorine dosing, making it a scalable solution.
APPLICATION 1
Chemical Unloading / Truckfill Station
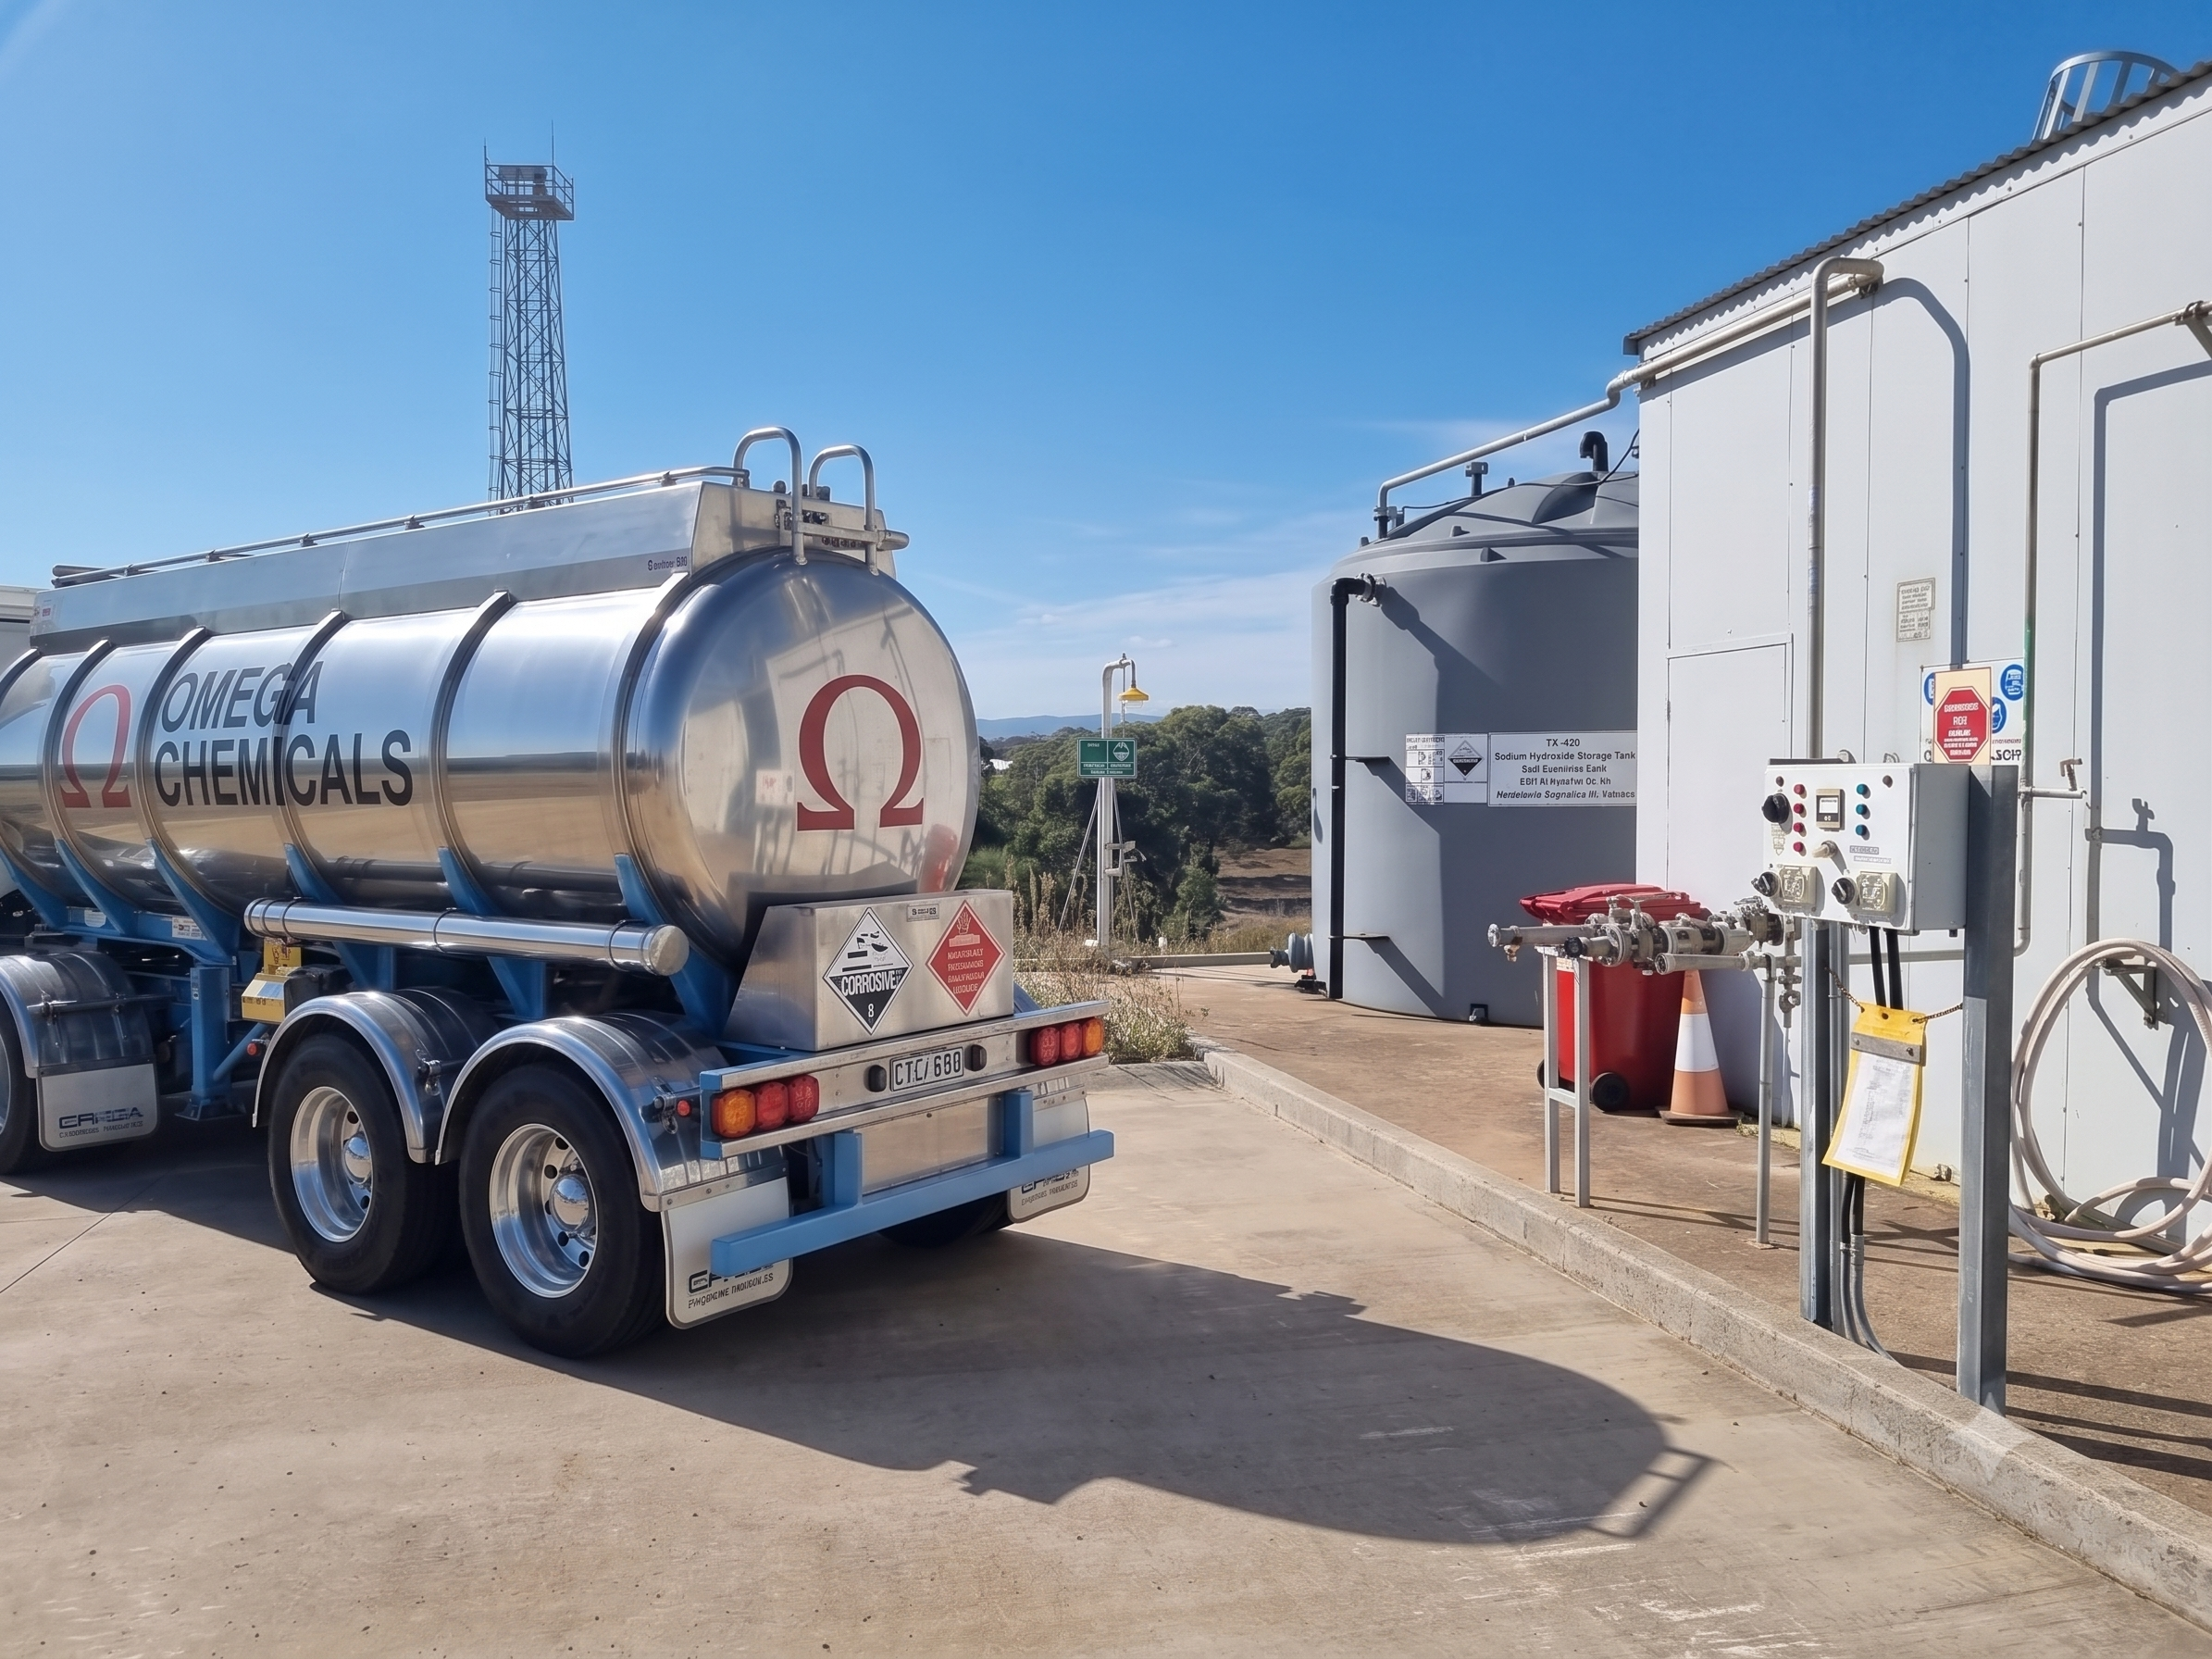
In the Chemical Unloading / Truckfill Station, the Multifunctional Controller provides automated control over the safe unloading of chemicals from trucks into storage tanks.
With its built-in alarms, power cut-off features, and remote monitoring capabilities, the controller ensures that each transfer is precisely managed, preventing overfilling and equipment damage.
This advanced control system reduces the need for manual intervention, enhancing both safety and compliance with industrial standards during critical unloading operations.
APPLICATION 2
Chemical Transfer Station
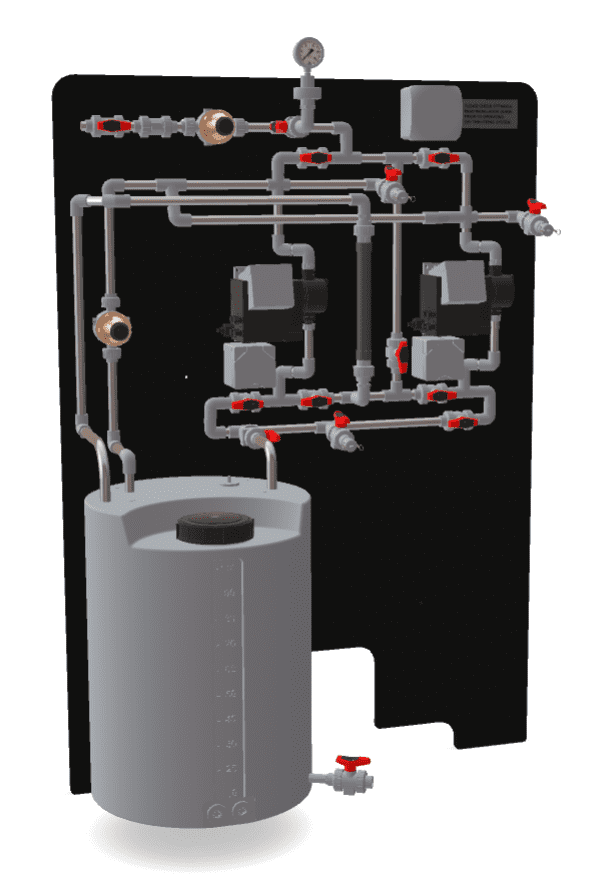
The Multifunctional Controller plays a central role in the Chemical Transfer Station, automating the transfer of chemicals between storage vessels with precision.
By integrating programmable refill levels and automated pump controls, the controller ensures smooth, error-free chemical transfers.
Its advanced features help optimise chemical levels, reduce manual intervention, and increase operational efficiency, making it a critical component in maintaining safety and reliability in high-volume chemical handling applications.
Contact Polymaster today about your liquid storage requirements